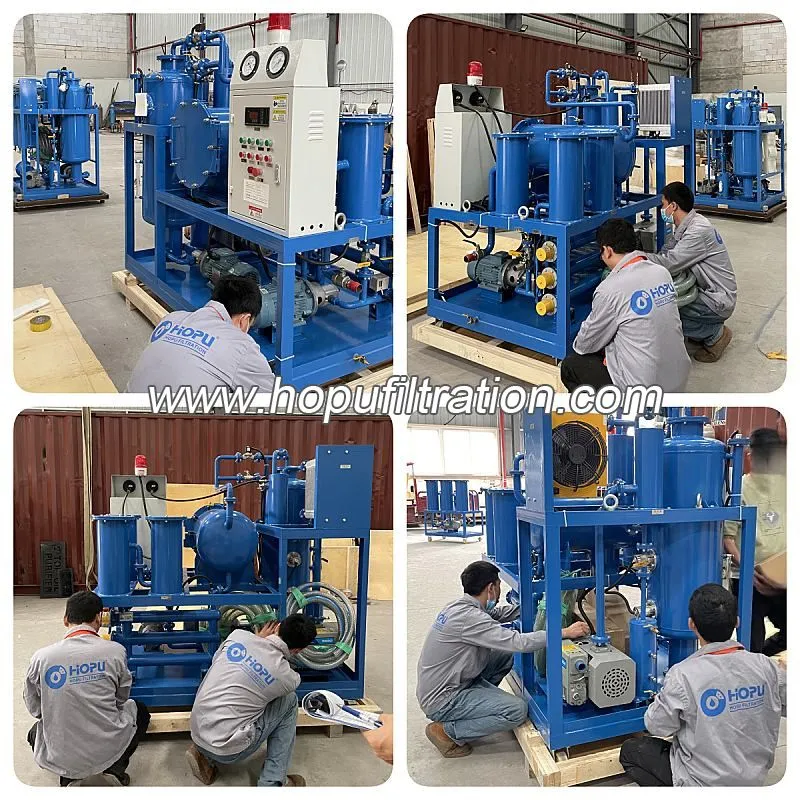
Turbine Oil Dehydration and Purification Machine Introduction:
In modern industrial systems, turbine oil serves as the "blood" of key equipment such as steam turbines and gas turbines, and its cleanliness and moisture content directly affect the safe operation and service life of the equipment. Traditional oil filtration equipment often fails to meet the increasingly stringent requirements for oil purification, while turbine oil vacuum oil purifier, with their innovative triple purification technology, are redefining the standards for industrial oil maintenance.
Turbine Oil Dehydration and Purification Mahcine is speacial for lube oil dewatering, and filtration. It is designed with coalescence separation system+ Vacuum dehydration unit, which is 20 times higher water removing efficiency than other vacuum type oil purifier. Double Dehydration effect can even remove 50% free water.
Turbine lube oil purifier has special patented technologies, set vacuum dehydration and coalescence separation engineering technology, cohesion technology, adsorption technology and sophisticated filtering technologies. Under high vacuum condition, the oil purifier can remove the water, gas and impurities in the oil quickly and reliably, increasing break emulsification ability, and comprehensively improve the quality of the oil to achieve online operation. It can remove water without stopping the machine, so that the waste oil to new oil standard, easy to operate .
Such as power plants, steam lubes during the long running, moisture, dust and solid particles of impurities inevitably mixed in the lube oil due to a variety of complex reasons,which accelerated oil oxidation, fueled bubble, fouling and sludge formation, causing seriously emulsified oil, leading oil and water difficult to separate, at last reducing oil lubrication, wear, heat dissipation, dispersion, cooling performance.At the same time, it causes the corrosion and wear of metal parts to affect the safe operation of the lube oil. Turbine Oil Dehydration and Filtration device is designed to solve the above problems.
Feature:
1.Integrates advantages of gravity method, degasification method, coalescence separation method, vacuum separation, mechanical filtration into one. With the technology of vacuum drying and demulsification, it can separate a large mount of water from the oil, even the micro quantity of moisture. It is good at dewatering and demulsifying, which can make the turbid emulsified oil become clear.
2.Equipped with vacuum analytical evaporation system which can remove the micro quantity of water from the oil and ensure the water content index in the oil. It won’t change the physical and chemical property of the oil, and it can extend the oil service life.
3.Low working noise meets the environmental protection requirement.
4.Precise multi-stage filters can effectively remove all kinds of mechanical impurities, preciser one by one, big impurity holding capacity and long service life.
5. On-line processing of the turbine oil of the steam engine, gas turbine and water turbine
Core technological advantages
Coalescence separation filter element: a breakthrough in precision filtration innovation
HOPU turbine oil vacuum purifier adopts advanced coalescence separation filter technology, achieving a qualitative leap in impurity removal efficiency. This specially designed filter element, through a multi-layer composite structure, can effectively capture solid particles with diameters as small as 1 micron, including metal wear particles, oxidation products, and foreign pollutants. The agglomeration effect causes tiny water droplets to gradually aggregate into larger droplets on the surface of the filter element, creating ideal conditions for the subsequent vacuum dehydration process. Actual application data shows that the impurity removal efficiency of this system can reach over 99.5%, far higher than the 85-90% level of traditional filtration equipment.
Vacuum dehydration system: key technology for deep purification
The efficient vacuum dehydration system equipped with the equipment is the core of removing water from the oil. This system significantly reduces the boiling point of oil by creating a vacuum environment of -0.08 to -0.095MPa, and can achieve rapid evaporation of water under mild conditions of 40-60 ℃. This low-temperature treatment method not only avoids the damage of high temperature to oil performance, but also effectively removes three different forms of water: dissolved water, emulsified water, and free water. The water content of the processed turbine oil can be reduced to below 50ppm, reaching or even exceeding the new oil standard, ensuring reliable operation of the equipment under extreme working conditions.
Explosion proof safety system: a reliable guarantee for industrial environments
Considering the potential risks of flammability and explosion in industrial sites, the turbine oil vacuum filter is specially equipped with a comprehensive explosion-proof safety system. The equipment adopts explosion-proof motors, explosion-proof electrical control boxes, and anti-static designs, and is manufactured strictly in accordance with Ex d IIB T4 explosion-proof standards. The system is equipped with multiple safety interlock devices, including temperature monitoring, pressure protection, and liquid level alarm, to ensure automatic shutdown protection in any abnormal situation. This intrinsic safety design enables the equipment to operate safely in high-risk environments such as petrochemicals and coal mines, providing a solid guarantee for the safety production of enterprises.
Overall performance
The three core technologies of the turbine oil purifier work together to form a powerful comprehensive purification capability. Actual operating data shows that a single device can process 1000 liters of contaminated turbine oil (with a water content of 1000ppm and impurity content NAS level 12) within 8 hours to a high-quality standard with a water content below 50ppm and cleanliness reaching NAS level 5. This efficient purification capability not only extends the service life of turbine oil by 3-5 times, but also significantly reduces equipment maintenance costs and downtime.
Technical Parameter:
| item |
unit |
TY-10 |
TY-20 |
TY-30 |
TY-50 |
TY-100 |
TY-150 |
TY-200 |
| Flow rate |
L/h |
600 |
1200 |
1800 |
3000 |
6000 |
9000 |
12000 |
| Working vacuum degree |
Mpa |
0.06 ~ 0.095 |
| Working pressure |
Mpa |
≤0.3 |
| Running temperature |
℃ |
40 ~ 70(the temperature of turbomachine below 55℃) |
| Heating power(Optional) |
KW |
14 |
16 |
18 |
30 |
45 |
55 |
60 |
| Total power |
KW |
16 |
18 |
20 |
33 |
48 |
61 |
71 |
| Inlet/outlet caliber |
mm |
φ25 |
φ25 |
φ25 |
φ32 |
φ42 |
φ50 |
φ50 |
| Size |
L |
mm |
1280 |
1350 |
1350 |
100 |
1500 |
1500 |
1600 |
| W |
mm |
750 |
900 |
950 |
950 |
1000 |
1200 |
1350 |
| H |
mm |
1450 |
1450 |
1500 |
1600 |
1650 |
1800 |
1800 |
| Weight |
Kg |
320 |
400 |
420 |
450 |
750 |
800 |
900 |
Your inquiry will be replied within 12 hours.
Please contact for more technical details and latest price